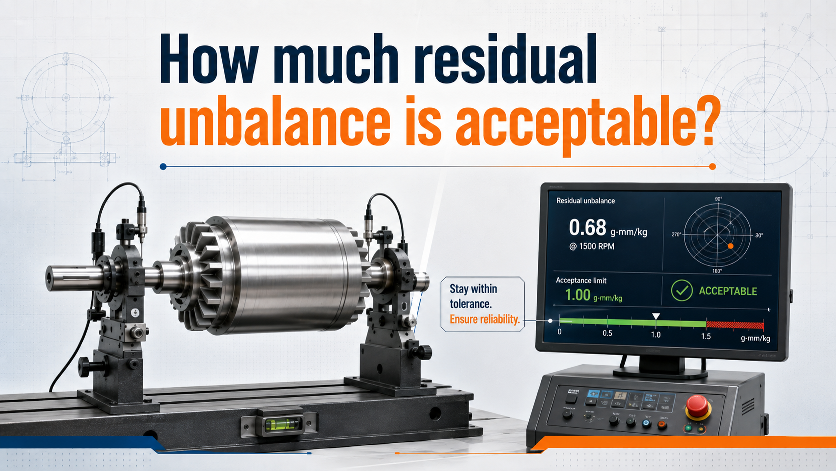
There is no single acceptable residual-unbalance value for every rotor. A remaining unbalance of 10 g·mm may be extremely small for one rotor and unacceptable for another. The tolerance must be related to rotor mass, speed, balance requirement and correction-plane allocation.
Residual unbalance is a moment
Unbalance is normally expressed as mass × radius, for example g·mm. A 10 g correction at 100 mm radius represents 1000 g·mm. The same unbalance moment could also be represented by 5 g at 200 mm radius.
Use specific residual unbalance
Specific residual unbalance normalises the unbalance by rotor mass. For a balance quality grade G:
eper (µm) ≈ 9549 × G / n
where n is the reference speed in r/min. Total permissible residual unbalance is then:
Uper (g·mm) = eper (µm) × rotor mass (kg)
Example: 80 kg fan rotor at 1450 r/min, G6.3
Specific permissible residual unbalance is approximately 41.5 µm. Multiplying by 80 kg gives a total permissible residual unbalance of about 3320 g·mm.
If that entire amount were represented at a 250 mm radius in one plane, it would correspond to about 13.3 g. A real two-plane tolerance must be allocated properly between the relevant planes, so this “equivalent mass” is only an illustration.
Why “remaining grams” is a poor acceptance statement
Correction mass without radius is incomplete. Saying “the rotor has 2 g left” does not tell you whether that 2 g is at 25 mm or 500 mm radius. The unbalance moment differs by a factor of twenty.
Why machine residual and installed vibration are not the same
Residual unbalance is a rotor property under the specified balance condition. Installed vibration is a system response. Bearings, support stiffness, resonance, alignment, fluid forces and assembly eccentricity can all affect the vibration measured after installation.
What acceptance basis should be used?
- Use the OEM or contract tolerance if one exists.
- Otherwise select a defensible ISO balance grade for the rotor duty.
- Use the appropriate reference speed and rotor mass.
- Allocate the permissible residual unbalance to the required tolerance or correction planes.
- Confirm the balancing process and tooling can resolve the required value repeatably.
Do not chase a number below process repeatability
If removing and reinstalling the rotor changes the reading by more than the stated tolerance, the process is not capable of proving that tolerance. Tooling, journals, shaft seating, key condition and measurement uncertainty must then be improved or the requirement reconsidered.
For grade selection, see What ISO 21940 balancing grade should I specify?